Arc interpretation error? (G3 / G2)

From the original Synthetos forum (2011–2025)

Started by borisw37 on in TinyG Support. 1 reply, last activity Jan 18, 2017.

#

I've been using tinyG w/ ChilliPeppr for a few weeks now running code generated by HSM works.
Yesterday I had a "tool crash" luckily just a gouge into soft wood.
I traced it to the following lines of gcode:

N12 G0 X48.224 Y-49.76
N13 Z5.
N14 Z2.
N15 G1 Z0.625 F300.
N16 G18 G2 X48.807 Z-0.008 R0.635
N17 G3 X54.236 Z-5.715 R5.715 F400.
N18 G1 X54.237 Z-6.35
....

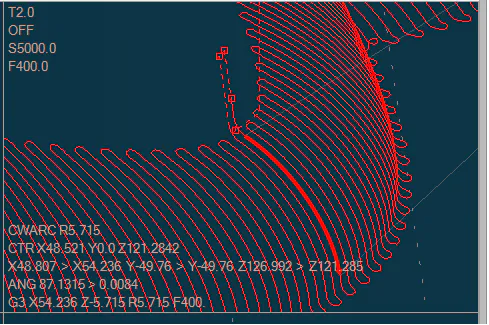
The N15 G3 Command caused a "concave" movement of the tool as opposed to convex.
I've attached two images:
one from ChilliPeppr showing the concave arc one from a G-code viewer showing the convex arc (how it should be)
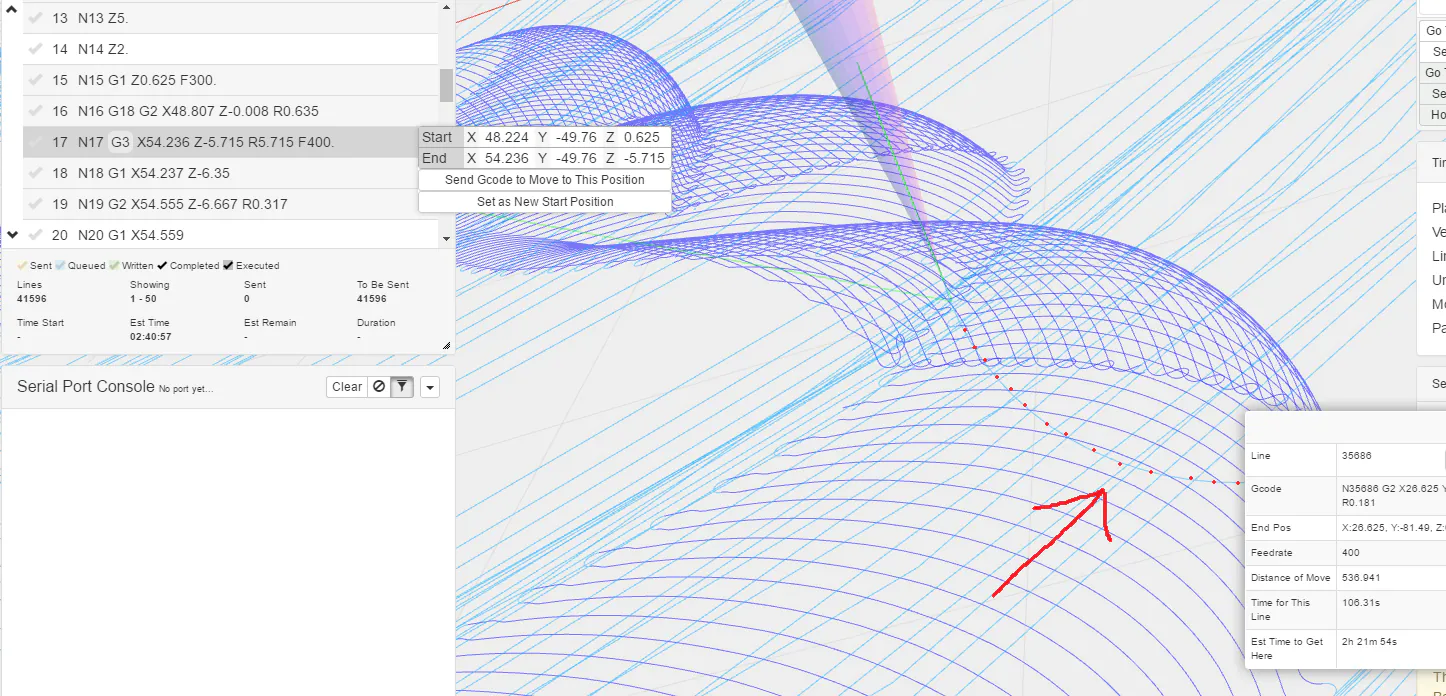
ChilliPeppr
Discrimiator g-code viewer

Is this a bug in tinyG, is it a toolpath generation or post processing bug? Toolpath simulates correctly in HSMworks.
*The same "crash" occured on the other side of the circular part (180 degrees around), other G2 and G3 commands seem to function just fine.

Thank you,

Boris.

Staff #

I'll assume your tinyG is running Firmware 440.20.
It is the best at this, but there are still bug(s) related to arcs

Possible short term solutions
1. I can't tell for sure if your Gcode is mm or inch. If it is inch, try regenerating in mm; mm always works better. TinyG is native mm, so inch Gcode gets a lot of translation manipulation.
Recognizing the rather large numbers 48, 54, etc, I am guessing you are already mm (or have a really big machine)
2. To get your job done, try to generate the Gcode without arcs. I'm not sure if HSM has that option. You will get a Gcode file with arcs replaced by short G1 moves.

This topic is from the original forum (January 2017). Your reply starts a new discussion linked to it.

Reply

Different problem? Ask a new question

Back to TinyG Support or latest activity.